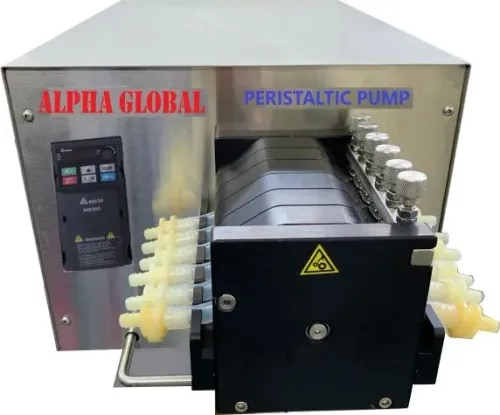
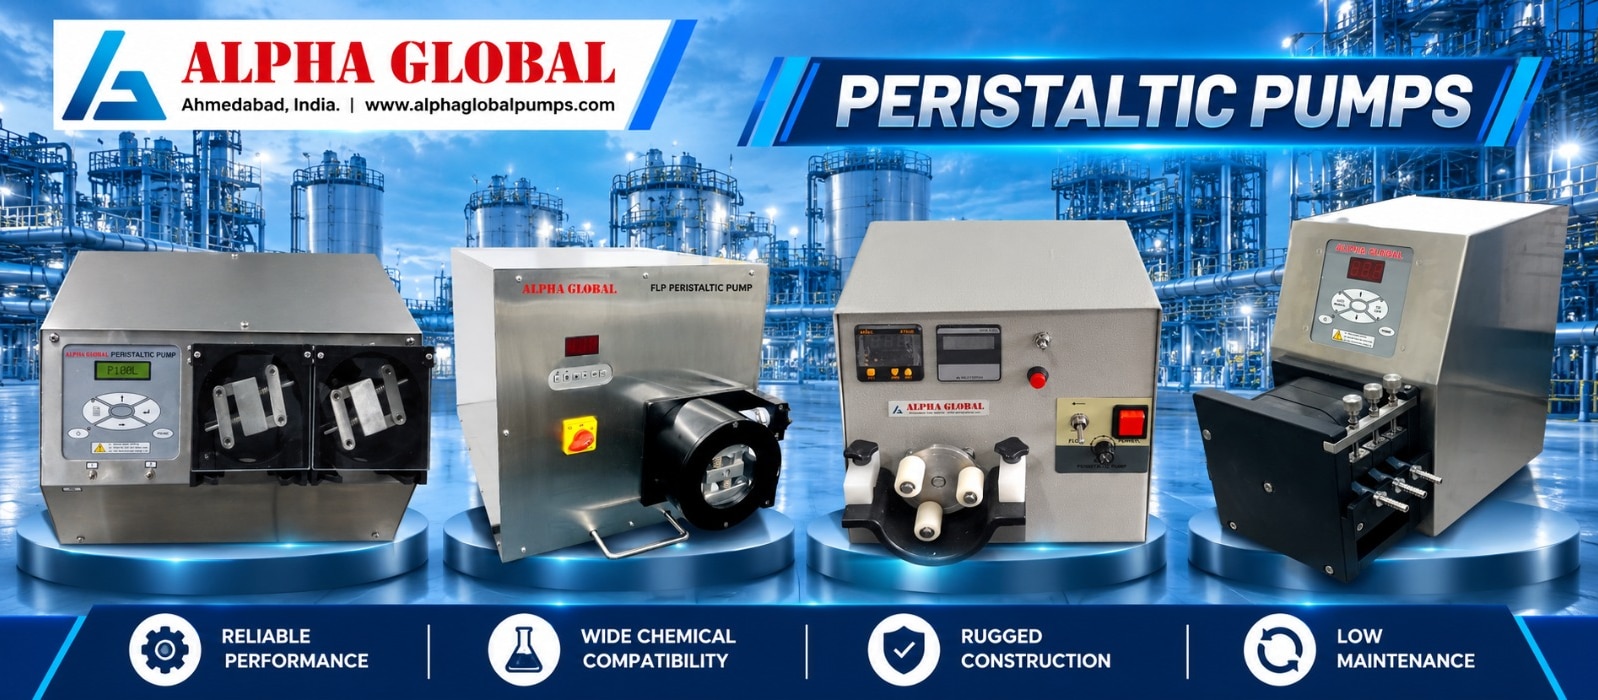
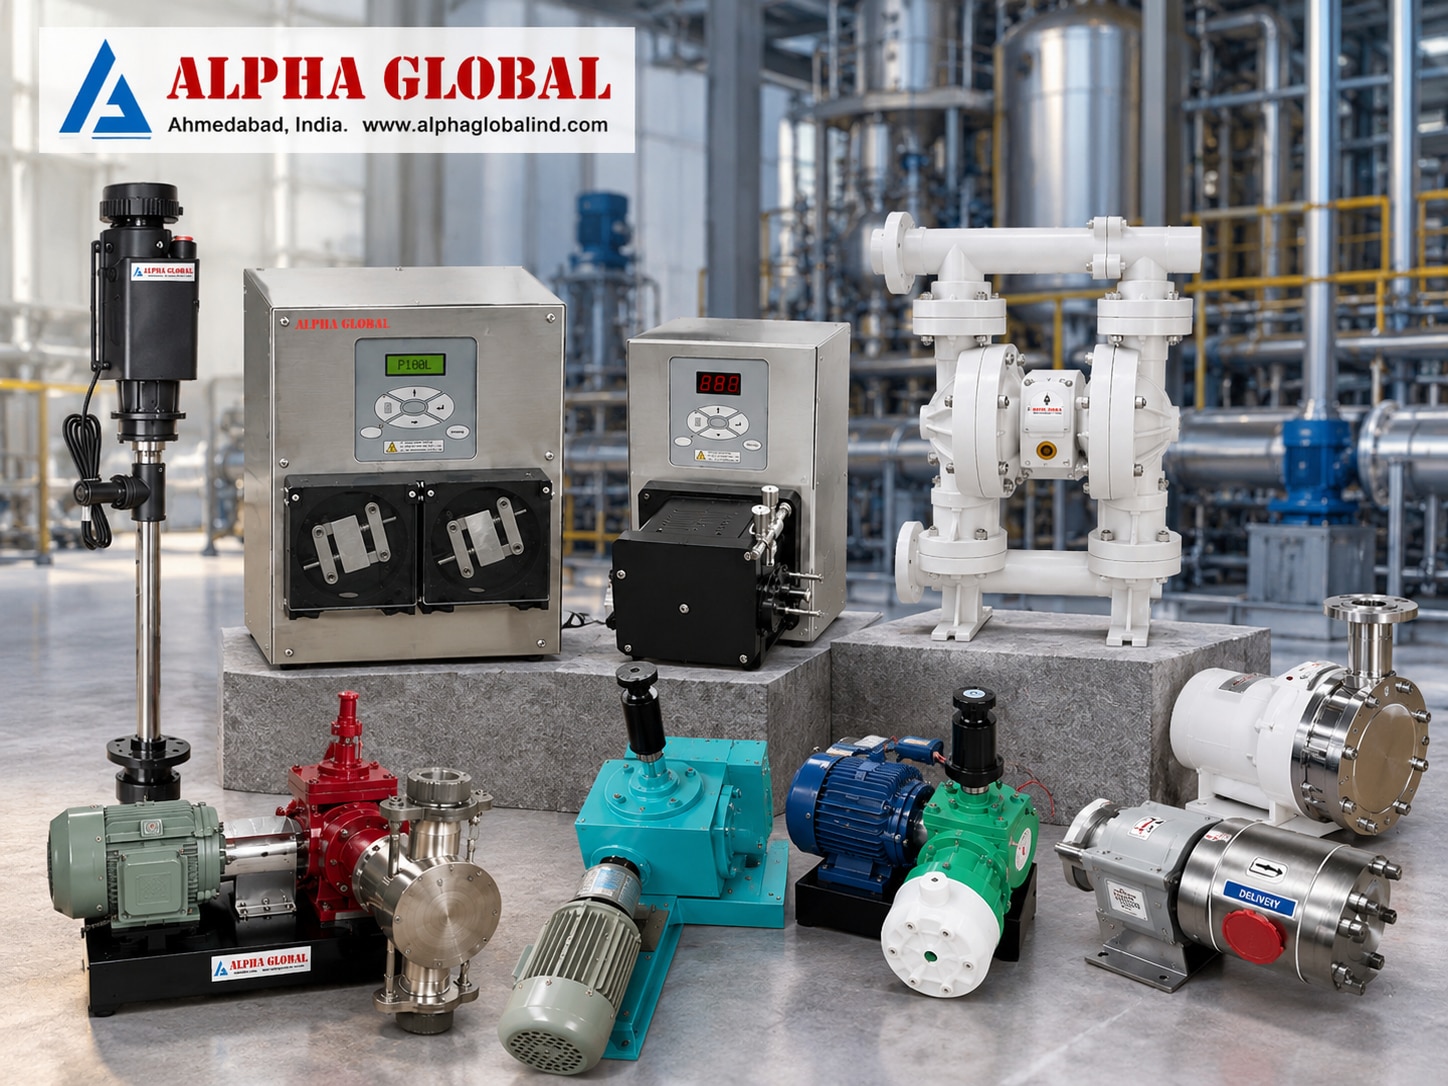
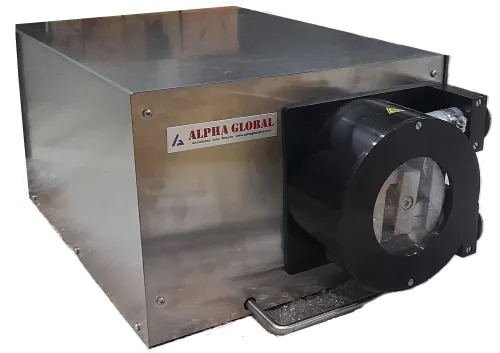
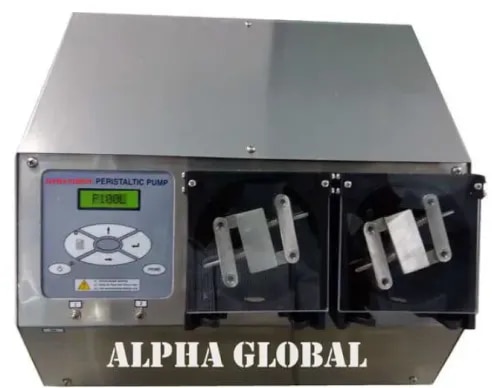
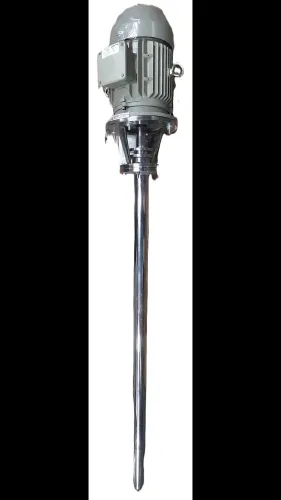
🔥Flame Proof Multi Channel Peristaltic Pumps ALPHA GLOBAL Flame Proof Multi Channel Peristaltic Pumps are designed for accurate, controlled and reliable liquid transfer and dosing in industrial environments where multiple liquid lines need to be handled simultaneously. These pumps combine the advantages of peristaltic pumping technology with a multi-channel configuration, making them suitable for chemical dosing, pharmaceutical processing, laboratory applications, water treatment, process industries and automated liquid handling systems. The pump operates through flexible tubing. Rollers compress the tubing in a controlled manner to move the liquid forward, while the pumped fluid remains inside the tube throughout the process. This helps minimize contamination and makes the pump suitable for applications where clean and controlled fluid handling is important. Flame-proof configurations are available for applications where the pumping equipment needs to be installed in potentially hazardous industrial environments. The exact hazardous-area suitability, certification, gas group and temperature classification should always be verified according to the selected model and site requirements. ⚙️ Key Features 🔹 Multi-channel pumping configuration for handling multiple liquid lines 🎯 Accurate and controlled liquid dosing 🧪 Fluid remains inside the flexible tubing during pumping 🔥 Flame-proof configuration options for suitable hazardous-area applications 🔧 Easy tubing replacement and maintenance 📏 Different channel and flow-rate configurations available ⚡ Suitable for automated and continuous industrial processes 🏭 Compact and practical industrial construction 🔄 Reversible pumping operation in suitable configurations 💧 Suitable for controlled transfer of different types of liquids 🔄 Working Principle Flame Proof Multi Channel Peristaltic Pumps work on the positive displacement principle. The flexible tube is positioned inside the pump head, and rotating rollers progressively compress the tube. As the rollers move, the compressed section travels along the tube and pushes the liquid forward. Once the roller passes, the tube returns to its original shape and draws additional liquid into the pumping section. Because the liquid comes into contact primarily with the selected tubing, the pump can provide a clean and controlled pumping process. Multiple channels allow several independent liquid lines to be operated using one common pumping arrangement. 🧪 Applications These multi-channel peristaltic pumps can be used across a wide range of industrial and technical applications, including: 🏭 Chemical processing 💊 Pharmaceutical manufacturing 🧪 Laboratory and research applications 💧 Water and wastewater treatment ⚗️ Chemical dosing systems 🛢️ Solvent and process liquid handling 🔬 Analytical instruments 💉 Reagent dosing 🏗️ Industrial automation 📦 OEM liquid-handling equipment 🎛️ Process-control systems 🔄 Multi-point dosing applications 🧴 Liquid dispensing systems ⚙️ Specialty chemical processing 🔥 Flame Proof Configuration For industrial environments where flammable gases or vapours may be present, flame-proof pump configurations can be considered according to the required hazardous-area classification. The applicable configuration should be selected based on: Hazardous-area classification Gas/vapour group Temperature classification Required certification Installation environment Operating conditions Local safety regulations Where required, the exact certification and suitability of the selected Flame Proof Multi Channel Peristaltic Pump should be confirmed before installation. 🎯 Advantages of Multi Channel Peristaltic Pumps Using a multi-channel arrangement can simplify applications where several liquids need to be transferred or dosed independently. Multiple Liquid Lines Multiple pumping channels can operate from a single integrated system, helping reduce the need for separate pump arrangements. Controlled Dosing The peristaltic pumping principle allows controlled movement of liquid, making it useful for dosing and dispensing applications. Reduced Fluid Contamination Since the liquid remains within the tubing, the pump provides a fluid path that can help reduce cross-contamination between the pumped liquid and mechanical components. Easy Maintenance Tubing replacement is generally straightforward, which can simplify routine maintenance and servicing. Flexible Pumping Different tubing materials and configurations can be selected depending on the liquid, flow rate, temperature and application requirements. 🏭 Flame Proof Multi Channel Peristaltic Pump Manufacturer in India ALPHA GLOBAL is engaged in manufacturing and supplying industrial pumping solutions for different process and liquid-handling applications. The company offers peristaltic pump configurations including fixed-speed, variable-speed, multi-channel and flame-proof options. The Flame Proof Multi Channel Peristaltic Pumps are suitable for industries requiring controlled liquid movement through multiple independent channels. Depending on the application, customers can select suitable pump configurations, tubing and drive arrangements based on required flow rate and operating conditions. 📋 How to Select the Right Pump? Before selecting a Flame Proof Multi Channel Peristaltic Pump, consider the following parameters: Number of pumping channels Required flow rate per channel Type of liquid Liquid viscosity Required tubing material Tubing internal diameter Operating temperature Operating pressure Required duty cycle Continuous or intermittent operation Hazardous-area classification Required flame-proof certification Installation environment Providing these details helps in selecting a suitable pump configuration for the intended application. ❓ Frequently Asked Questions What is a Flame Proof Multi Channel Peristaltic Pump? It is a multi-channel peristaltic pump designed for controlled liquid transfer or dosing through multiple independent tubing lines, with flame-proof configurations available for suitable hazardous-area applications. Can multiple liquids be pumped simultaneously? Yes. A multi-channel configuration is designed to provide multiple independent pumping channels, allowing different liquid lines to be handled simultaneously, subject to the selected model and configuration. Where are these pumps commonly used? They are commonly considered for chemical processing, pharmaceutical applications, laboratory systems, water treatment, industrial automation, reagent dosing and other controlled liquid-handling applications. What is the advantage of peristaltic pumping? The pumped liquid remains inside the flexible tubing, which can help provide a cleaner fluid path and reduce direct contact between the liquid and the pump's mechanical components. What information is required for pump selection? Important information includes required flow rate, number of channels, liquid characteristics, tubing size and material, temperature, viscosity, operating conditions and hazardous-area requirements where applicable. Are these pumps suitable for hazardous areas? Flame-proof configurations can be suitable for certain hazardous-area applications, but the exact model certification and hazardous-area classification must be verified before installation. ⭐ Why Choose ALPHA GLOBAL? ALPHA GLOBAL focuses on industrial pumping solutions designed around the specific requirements of liquid transfer, dosing and process applications. The company's peristaltic pump range provides different configurations for applications requiring: 🎯 Precise liquid dosing 🔄 Controlled fluid transfer 🧪 Clean tubing-based fluid handling 🏭 Industrial process integration 🔥 Suitable flame-proof configurations ⚙️ Multi-channel pumping 🔧 Practical maintenance Flame Proof Multi Channel Peristaltic Pumps Manufacturer & Supplier in India | ALPHA GLOBAL ALPHA GLOBAL Flame Proof Multi Channel Peristaltic Pumps are designed for controlled and accurate liquid transfer through multiple independent channels. These pumps are suitable for chemical dosing, pharmaceutical processing, water treatment, laboratory applications, industrial automation and process industries. With tubing-based fluid handling and flame-proof configuration options, they provide a practical solution for multi-point dosing and liquid-handling applications where reliable and controlled pumping is required.
Ahmedabad
08048034120
+918320946269
 Chat with us
 Chat with us
About Alpha Global - Industrial Pumps Manufacturer
Providing Best Solutions In Industrial Pumps...🏭
Products
Featured ProductsWhat We Do
Have any custom requirements?
Updates
Read What’s Latest
Testimonials
View All
Vijay Kumar, Kolkata, West Bengal
Alpha Global helped us select a suitable pumping solution for our industrial process. The team was professional, respons...
Read MoreSanjay Gupta, Indore, Madhya Pradesh
We purchased an industrial pump from Alpha Global for our manufacturing process and were satisfied with the overall expe...
Read MoreKiran Rao, Bengaluru, Karnataka
We had a good experience dealing with Alpha Global for our industrial pumping requirement. Their team provided useful te...
Read More
×
![]()